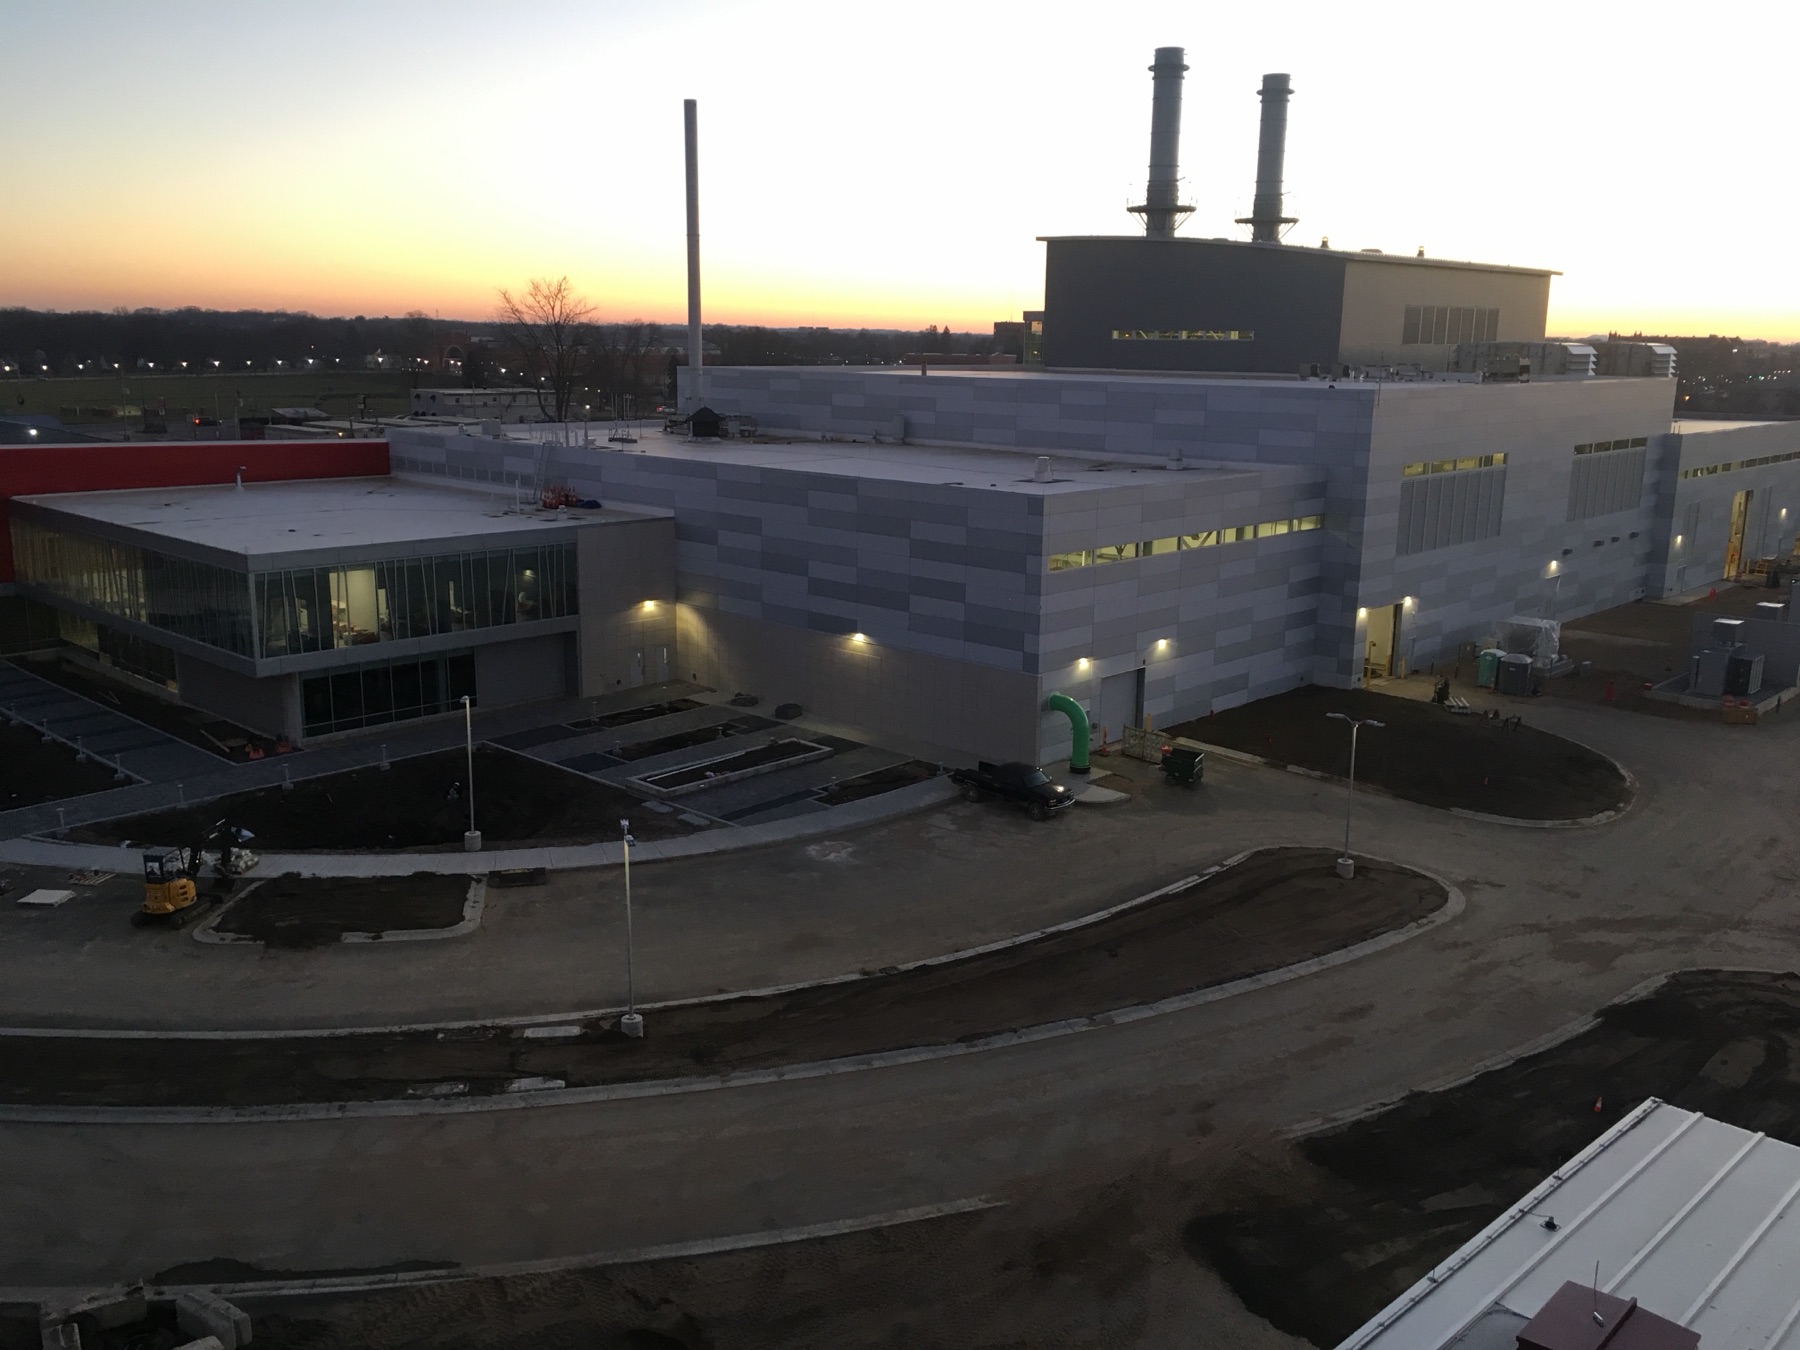
Compressor Station
Major Utility Company
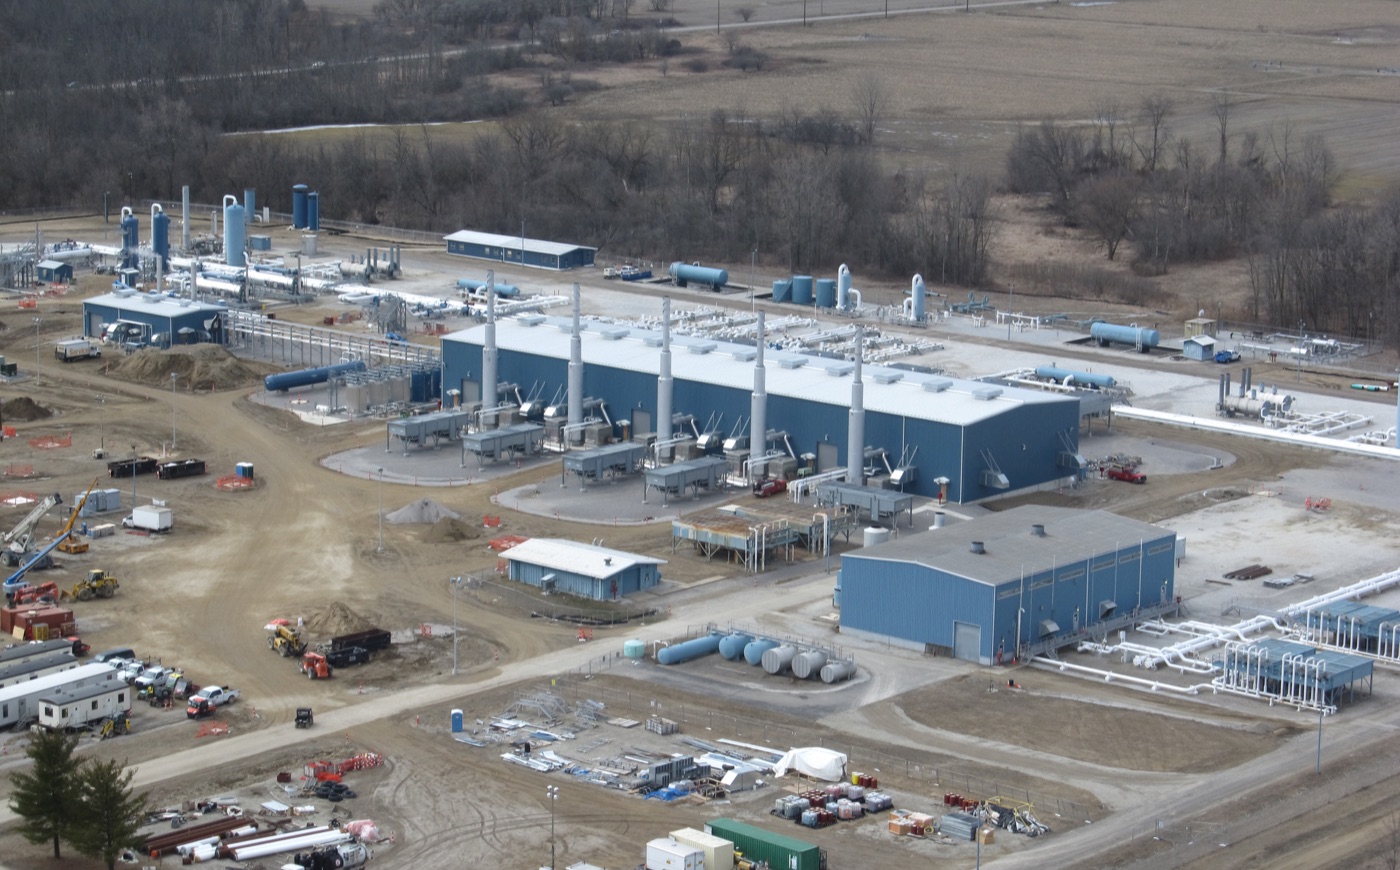
Taking a major utility plant offline for any duration of time is typically a carefully orchestrated operation. Delays create havoc and the costs that accompany them are enormous. For this reason, the standard practice when retrofitting pipelines is to leave extra length on spools being welded in the field. This extra length gives the installers a margin of error to work with, but measuring, cutting, fitting and prepping in the field also adds time to the schedule. Still, most contractors prefer this method because they aren’t using processes and technology that guarantee accuracy. If their measurements are wrong, a spool that’s cut too short for its tie-in point could add weeks of delay – and escalating costs – to a shutdown.
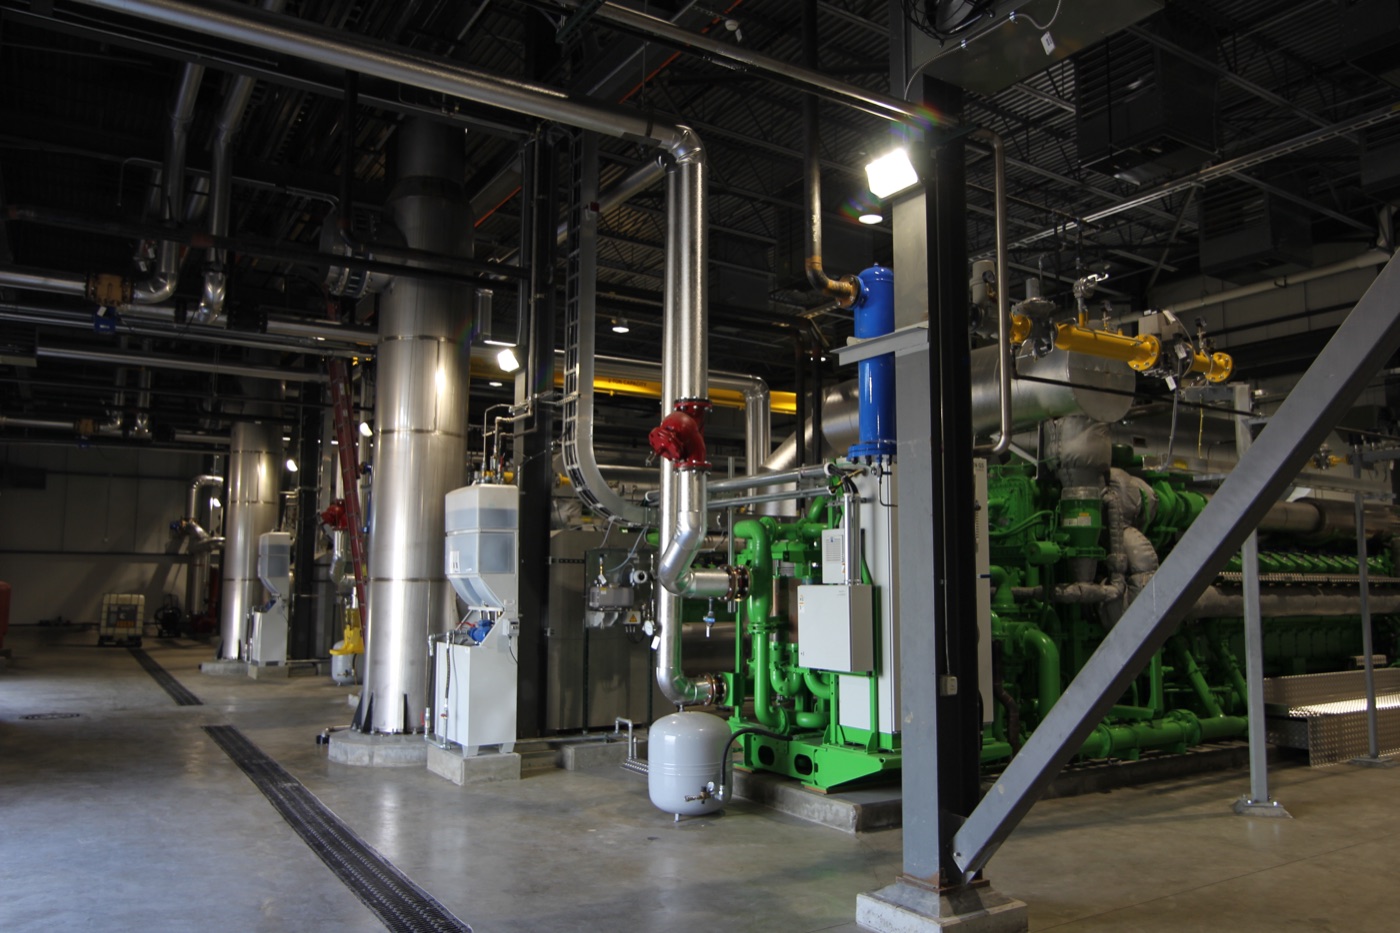
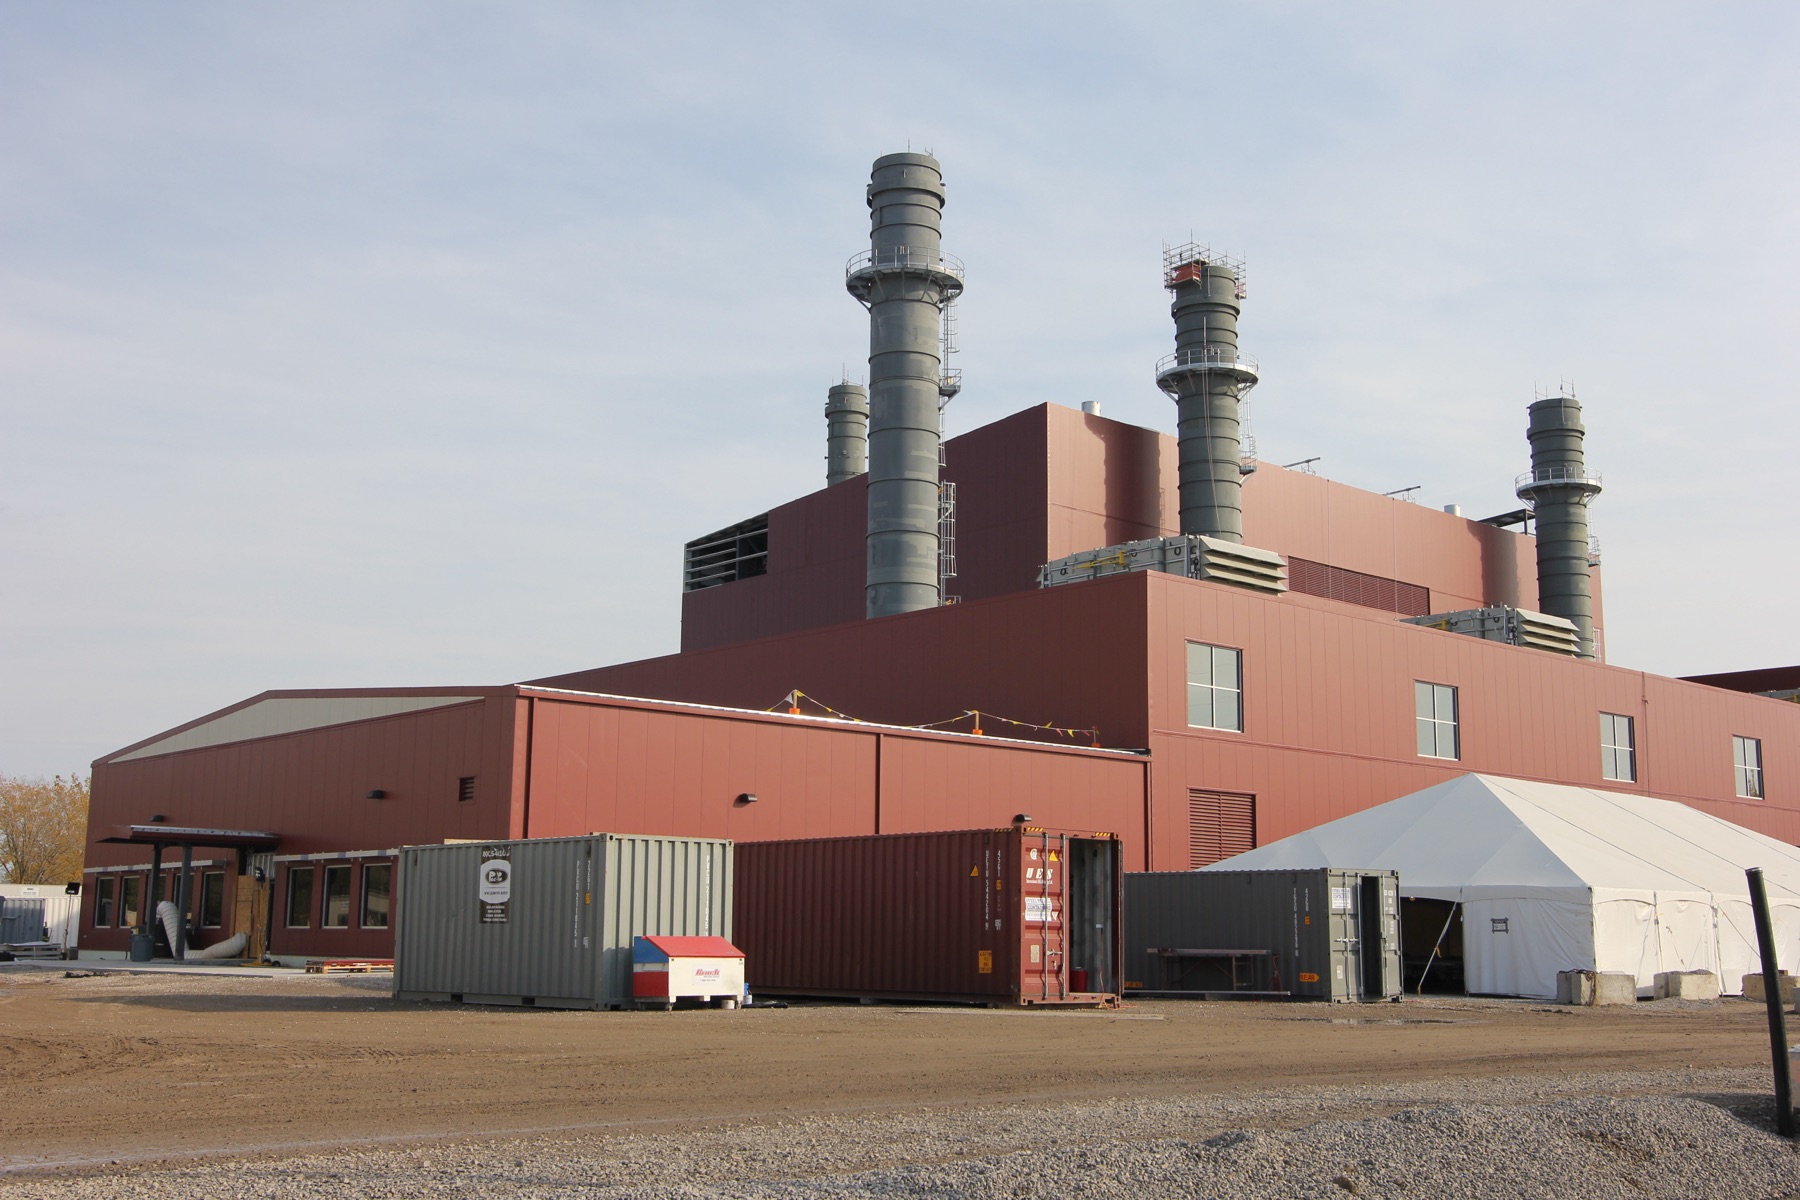
For installations requiring this level of accuracy, mechanical contractor Andy J. Egan Co., Inc. relies on its internal construction technology division for verification of precise measurements and layout at multiple points during the project schedule. For one recent, high-risk project, Egan precisely coordinated its suite of in-house services to replace a 97,000 lb. dry gas filter at a compressor station in just three days, with no field modifications or delays, and with the spool for critical tie-in point cut to exact length needed – an impossible task for most contractors.
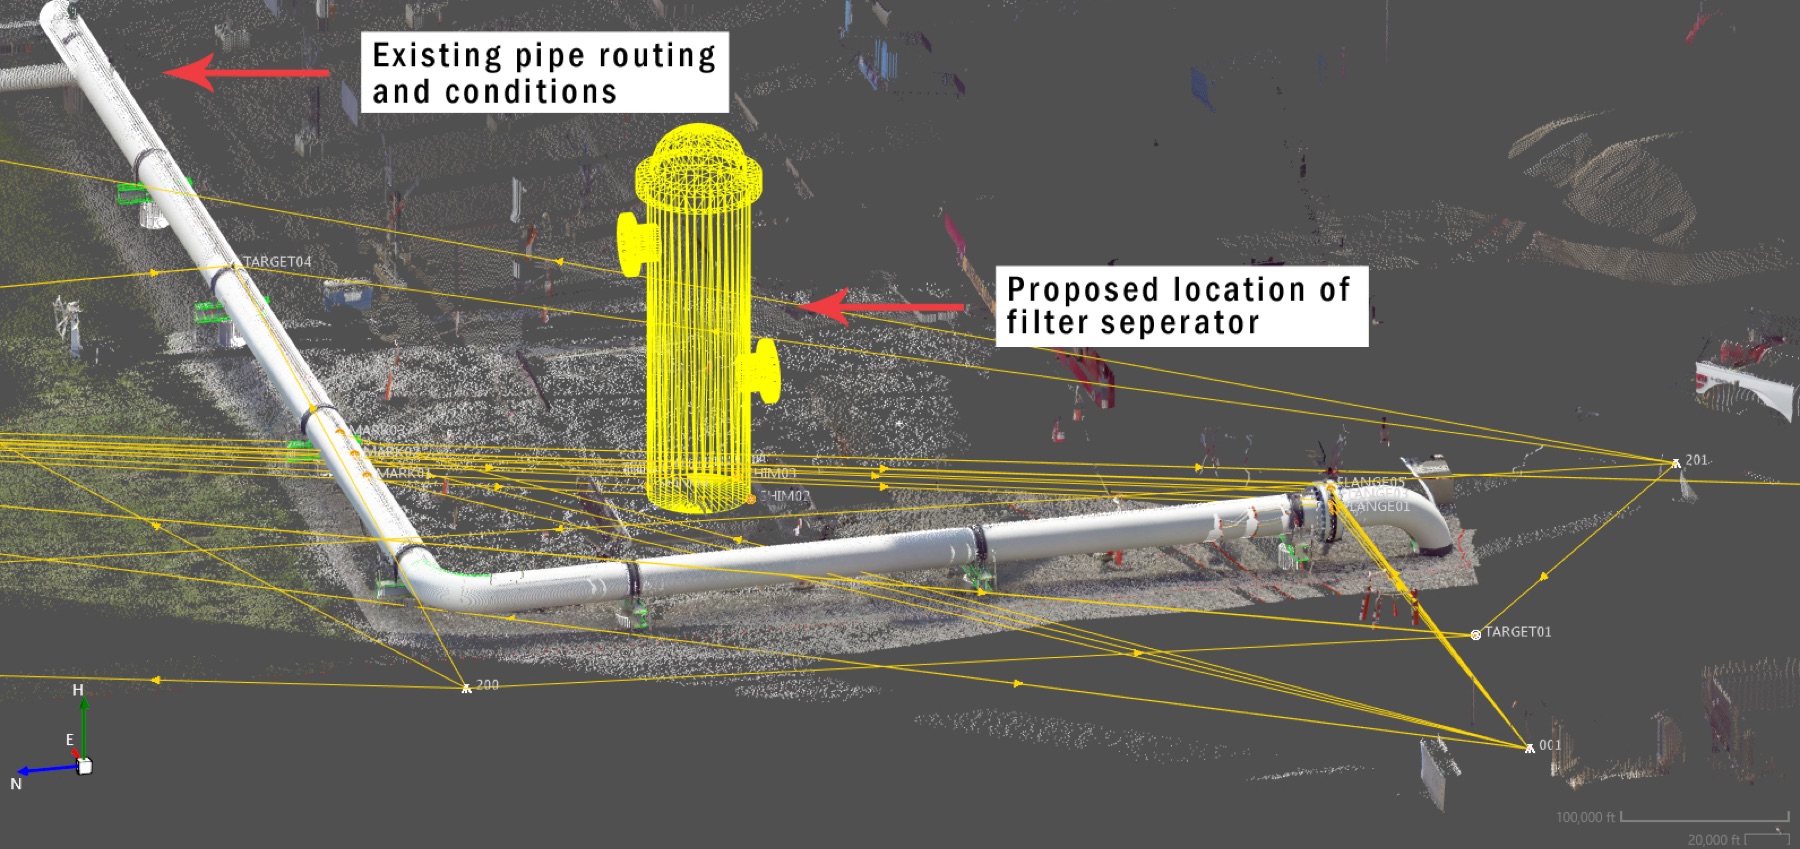
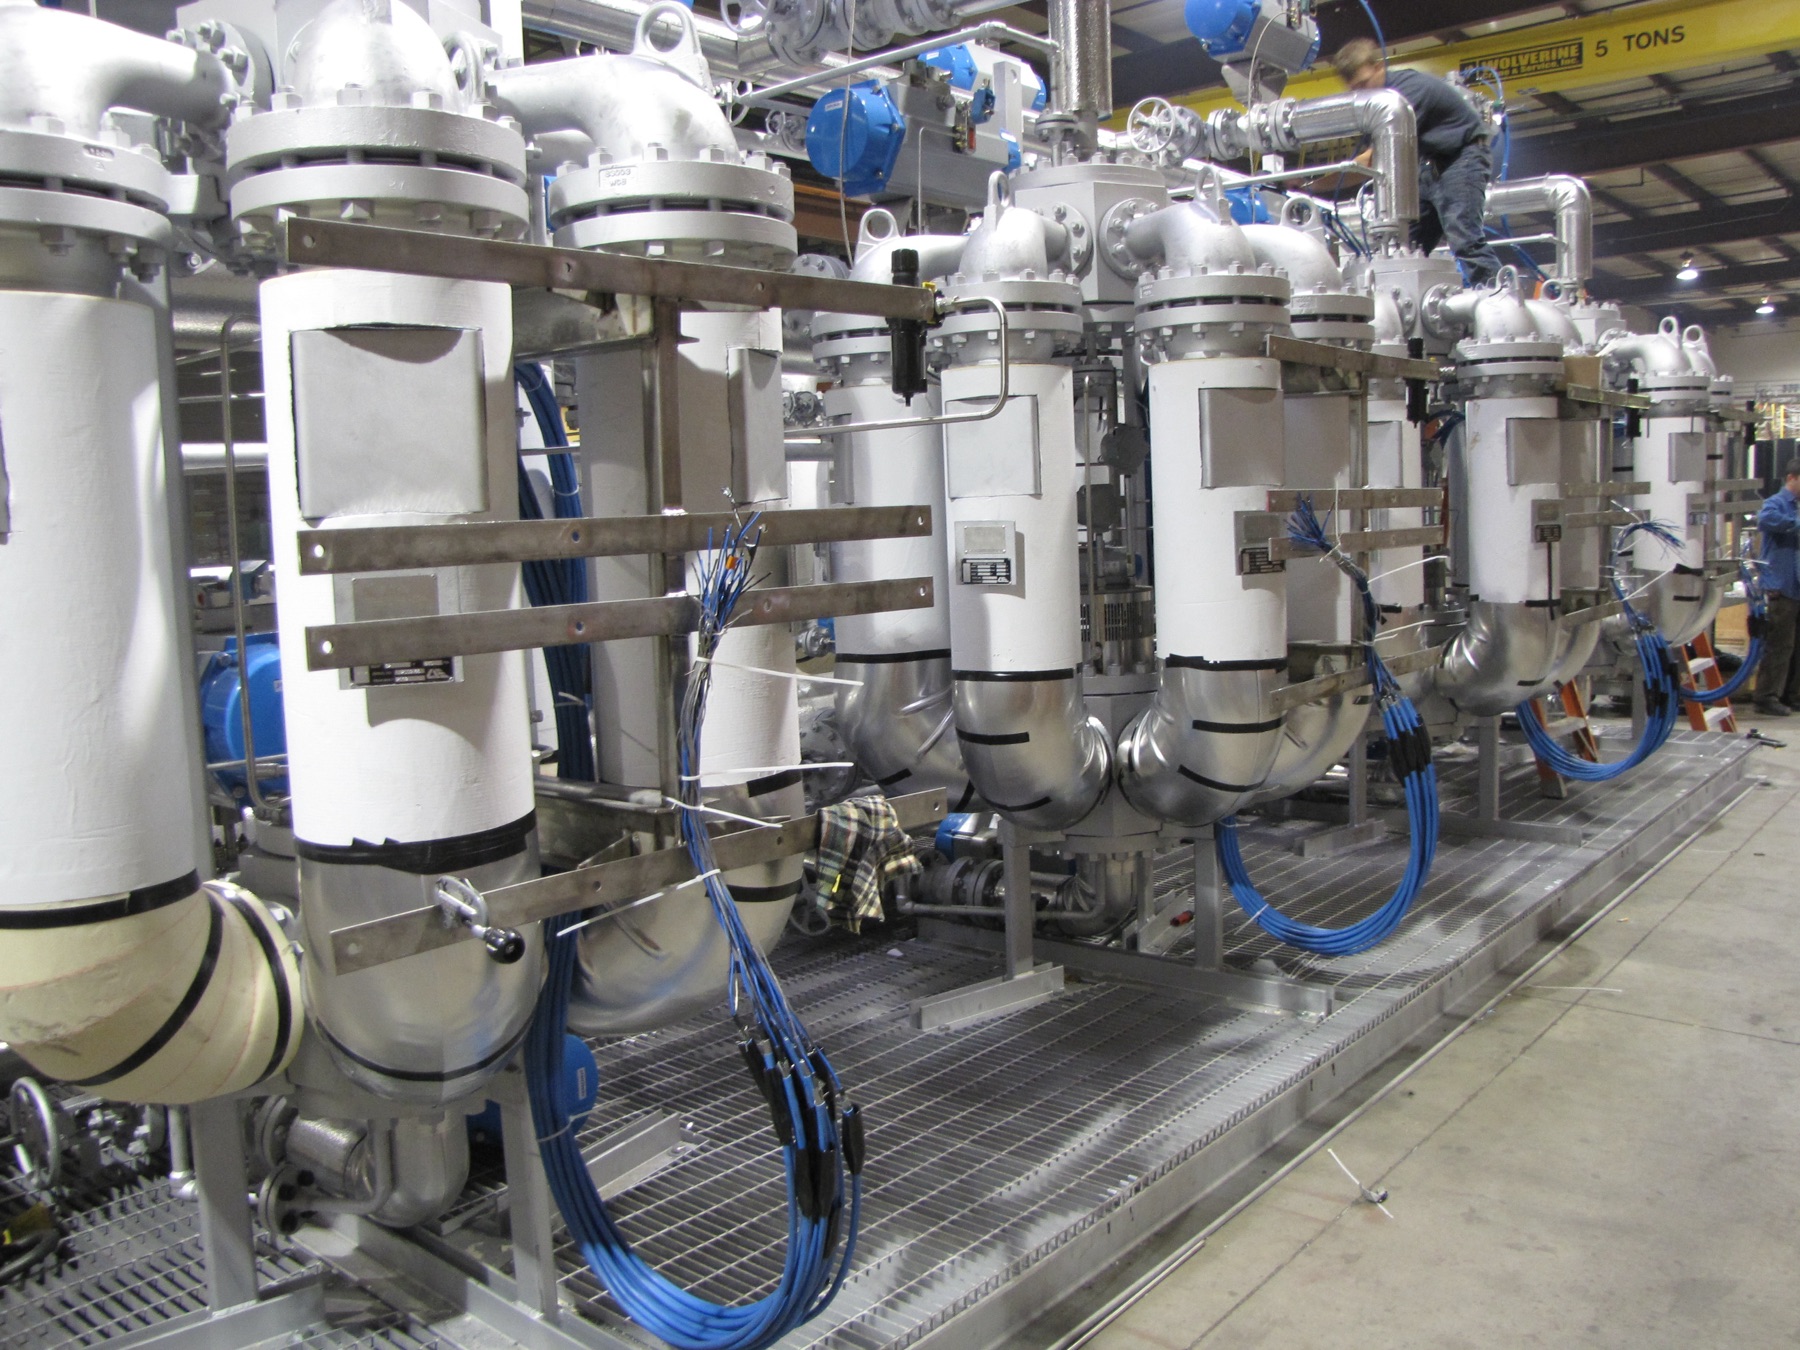
The pre-construction and fabrication phases of this project were key to its success and began weeks ahead of the install. The customer provided design drawings for the filter, which was “leftover” from another project site. Egan’s team set the filter on a concrete foundation that had been previously poured, then worked to verify existing conditions.
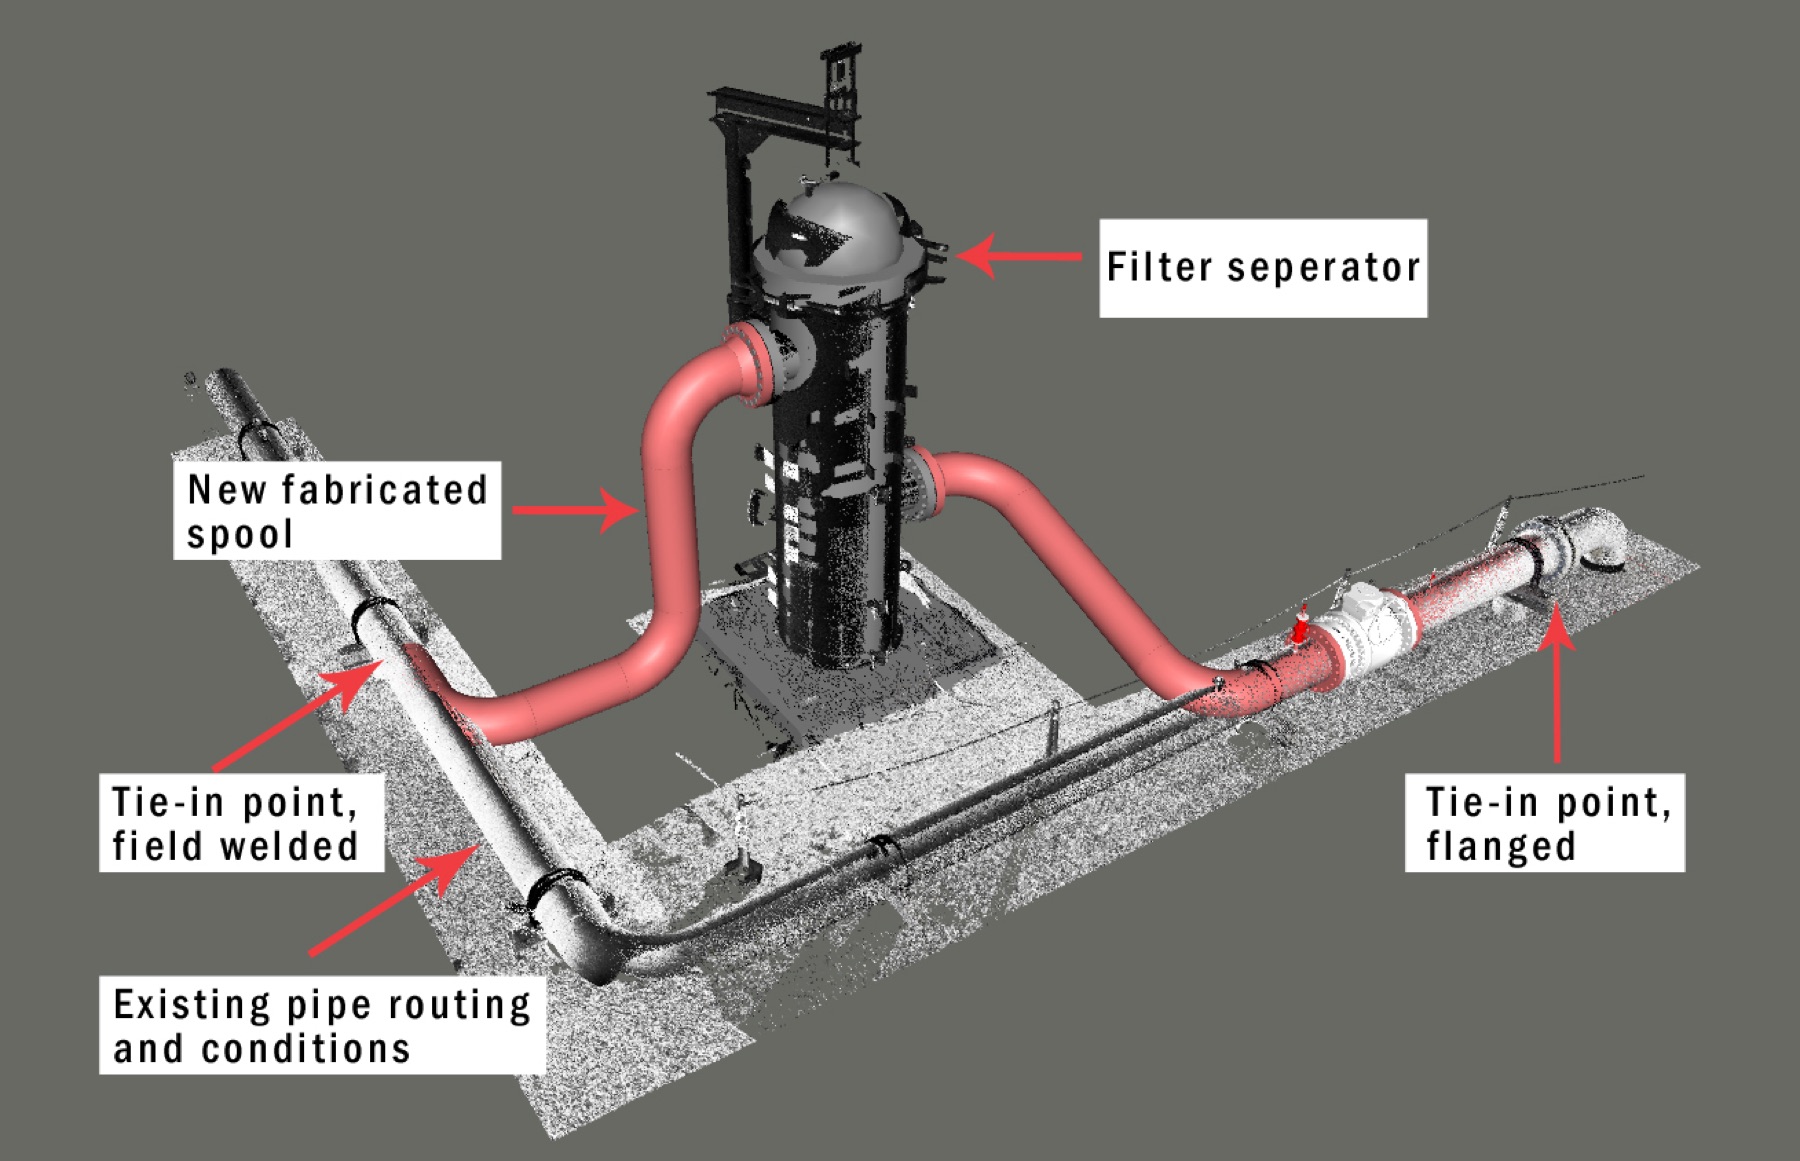
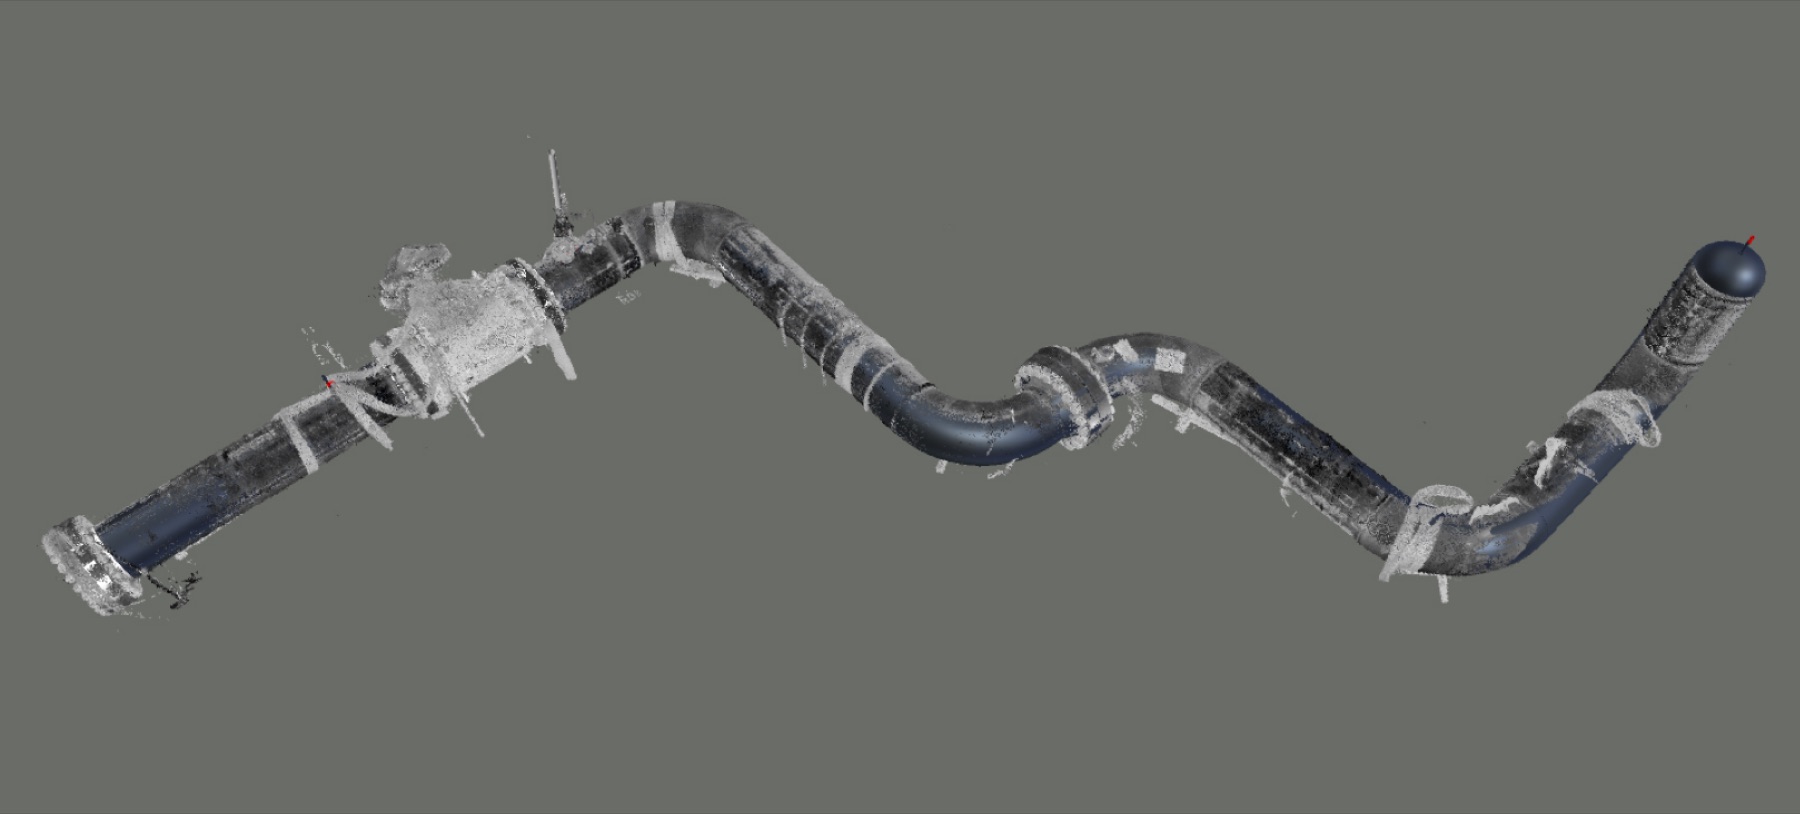
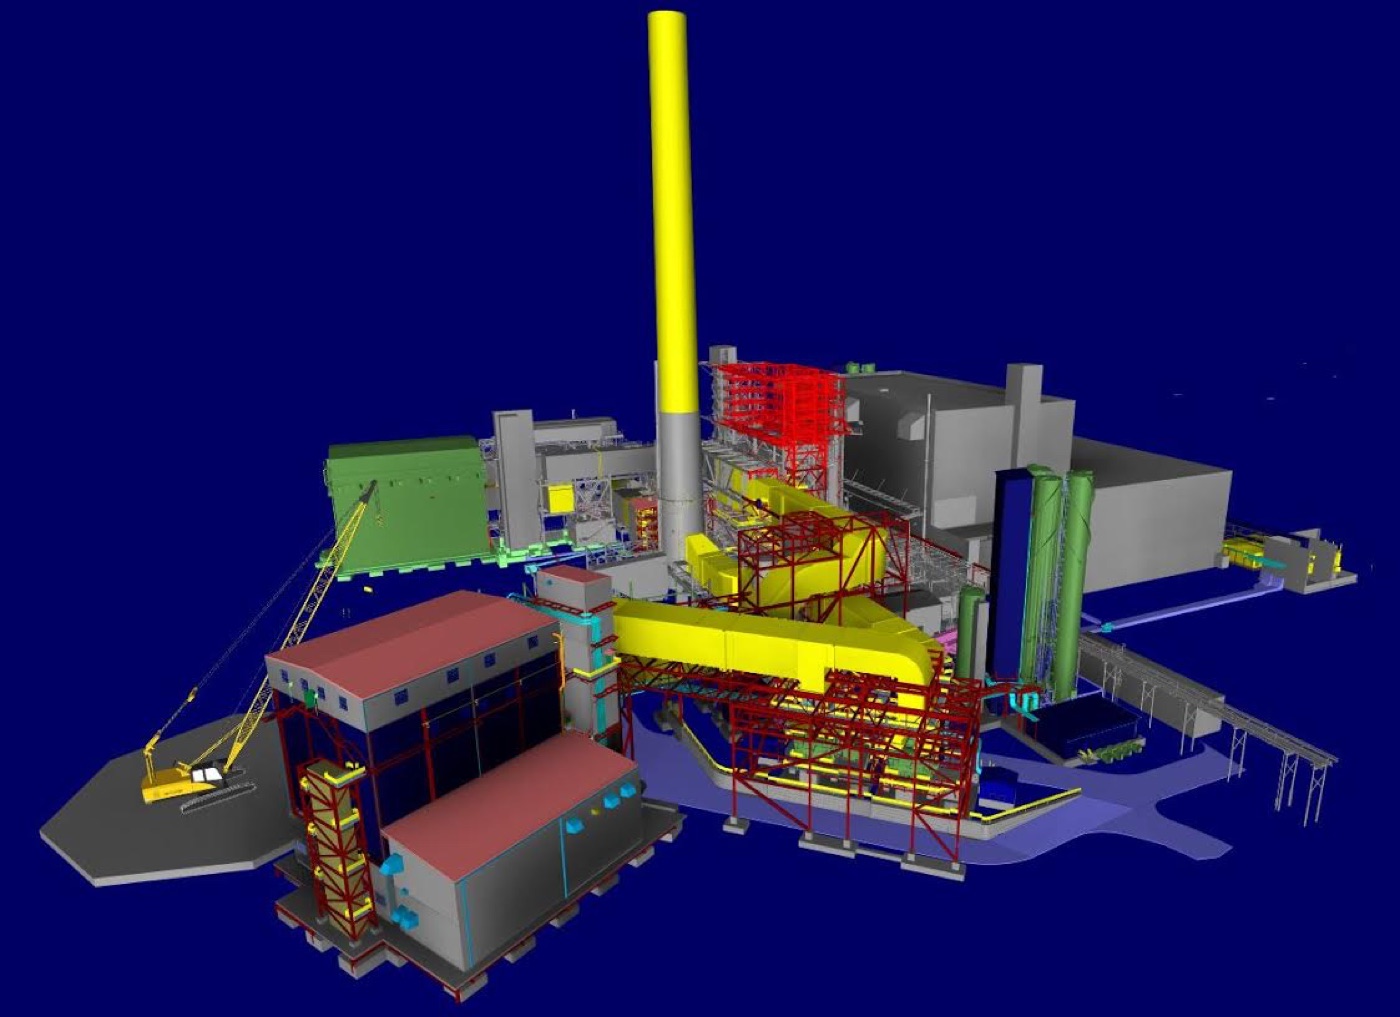
Even in the project’s early stages, verification was quicker and more accurate, setting the foundation for success. Egan scanned the filter and its fixed tie-in points, revealing the exact dimensions and angles of the onsite conditions. A key tie-in point required a unique 17.8 degree connection angle, which Egan’s internal BIM specialists were able to account for in the 3D coordinated model.
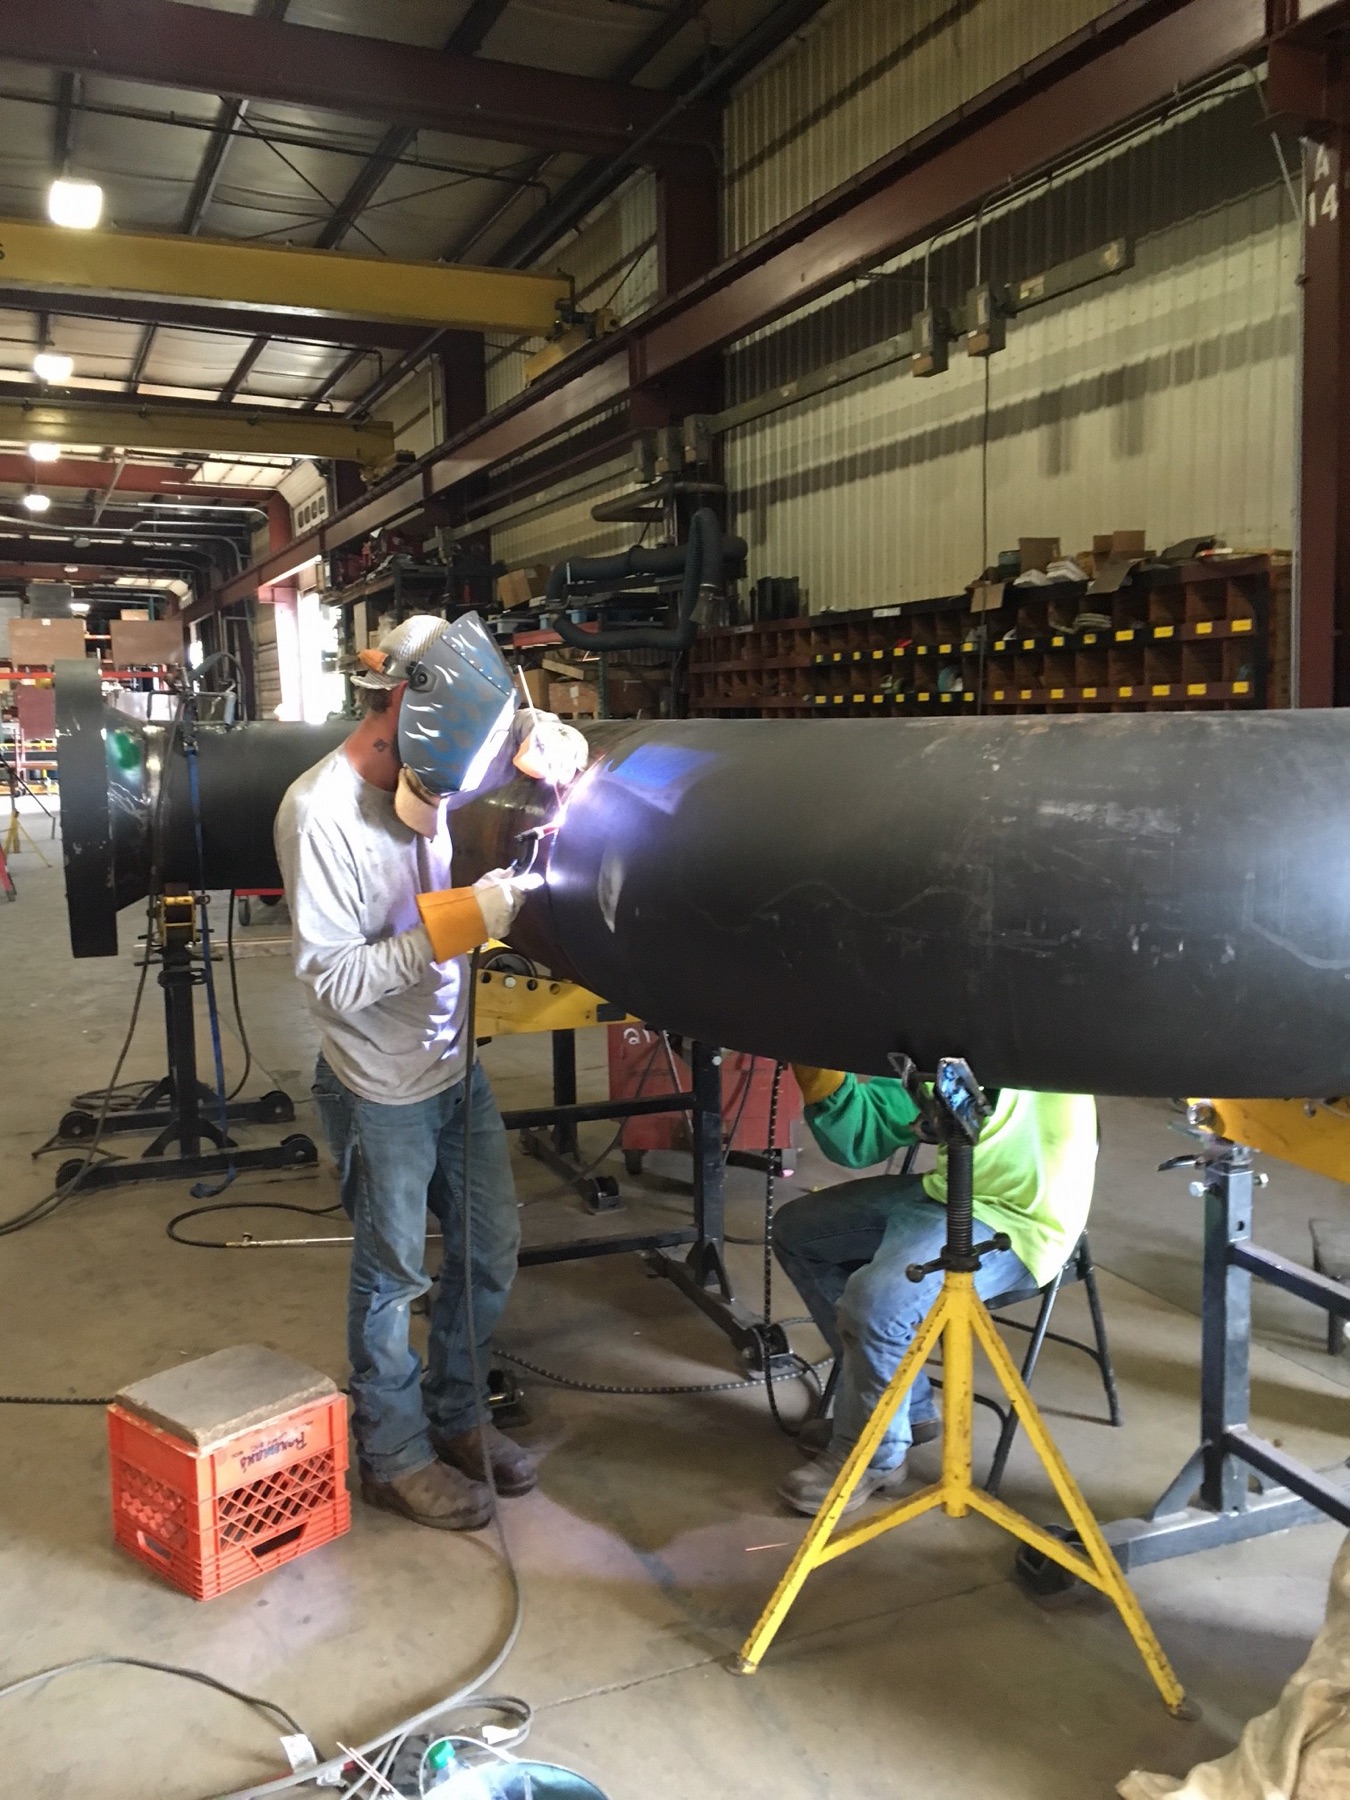
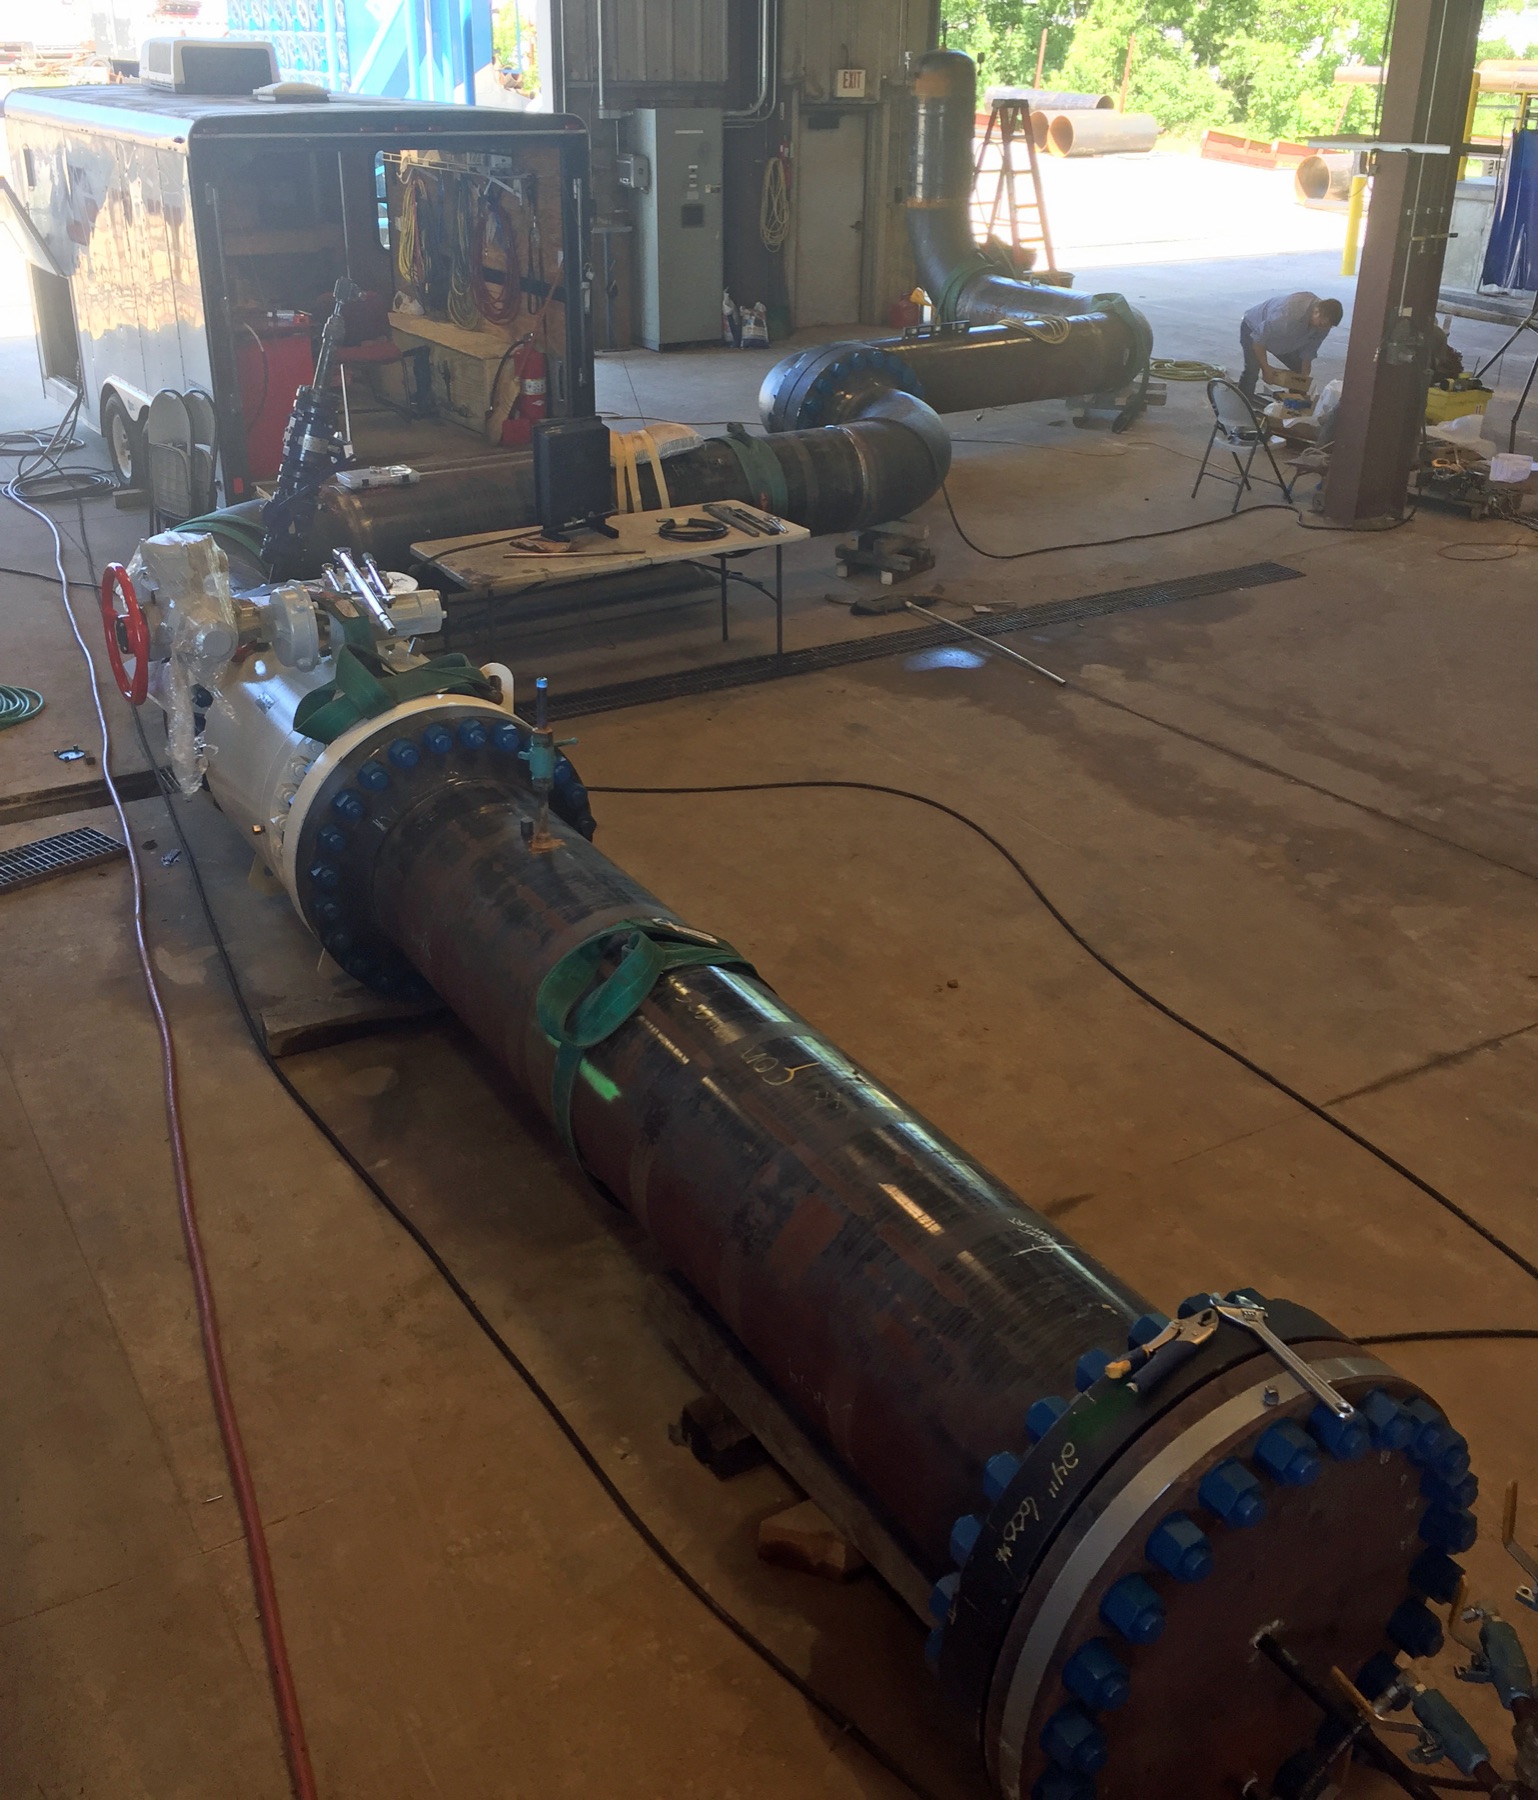
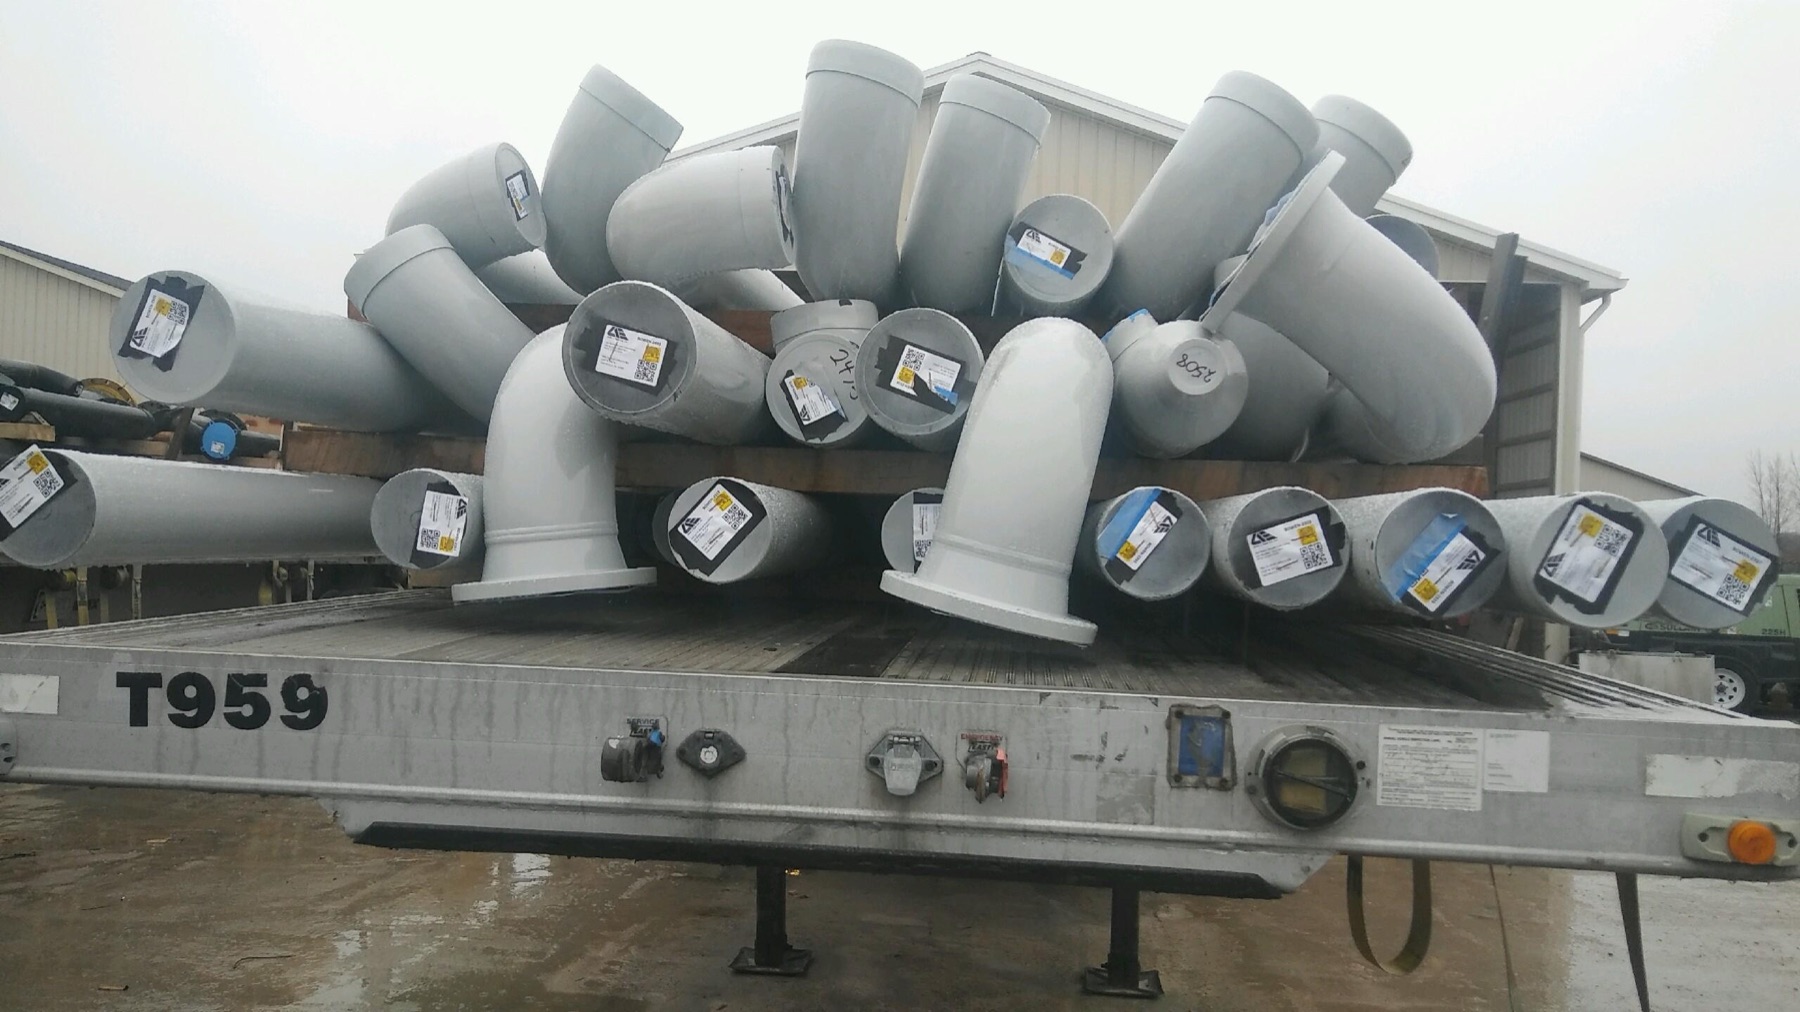
From the model, the project team generated spool drawings for fabrication. Egan’s certified welders then fabricated three 24-inch pipe spools with flanged joints that precisely aligned to the onsite connection points. As part of Egan’s quality assurance process, the spools underwent a final scan to verify dimensions prior to shipping, as well as complete hydrotesting in the fabrication shop.
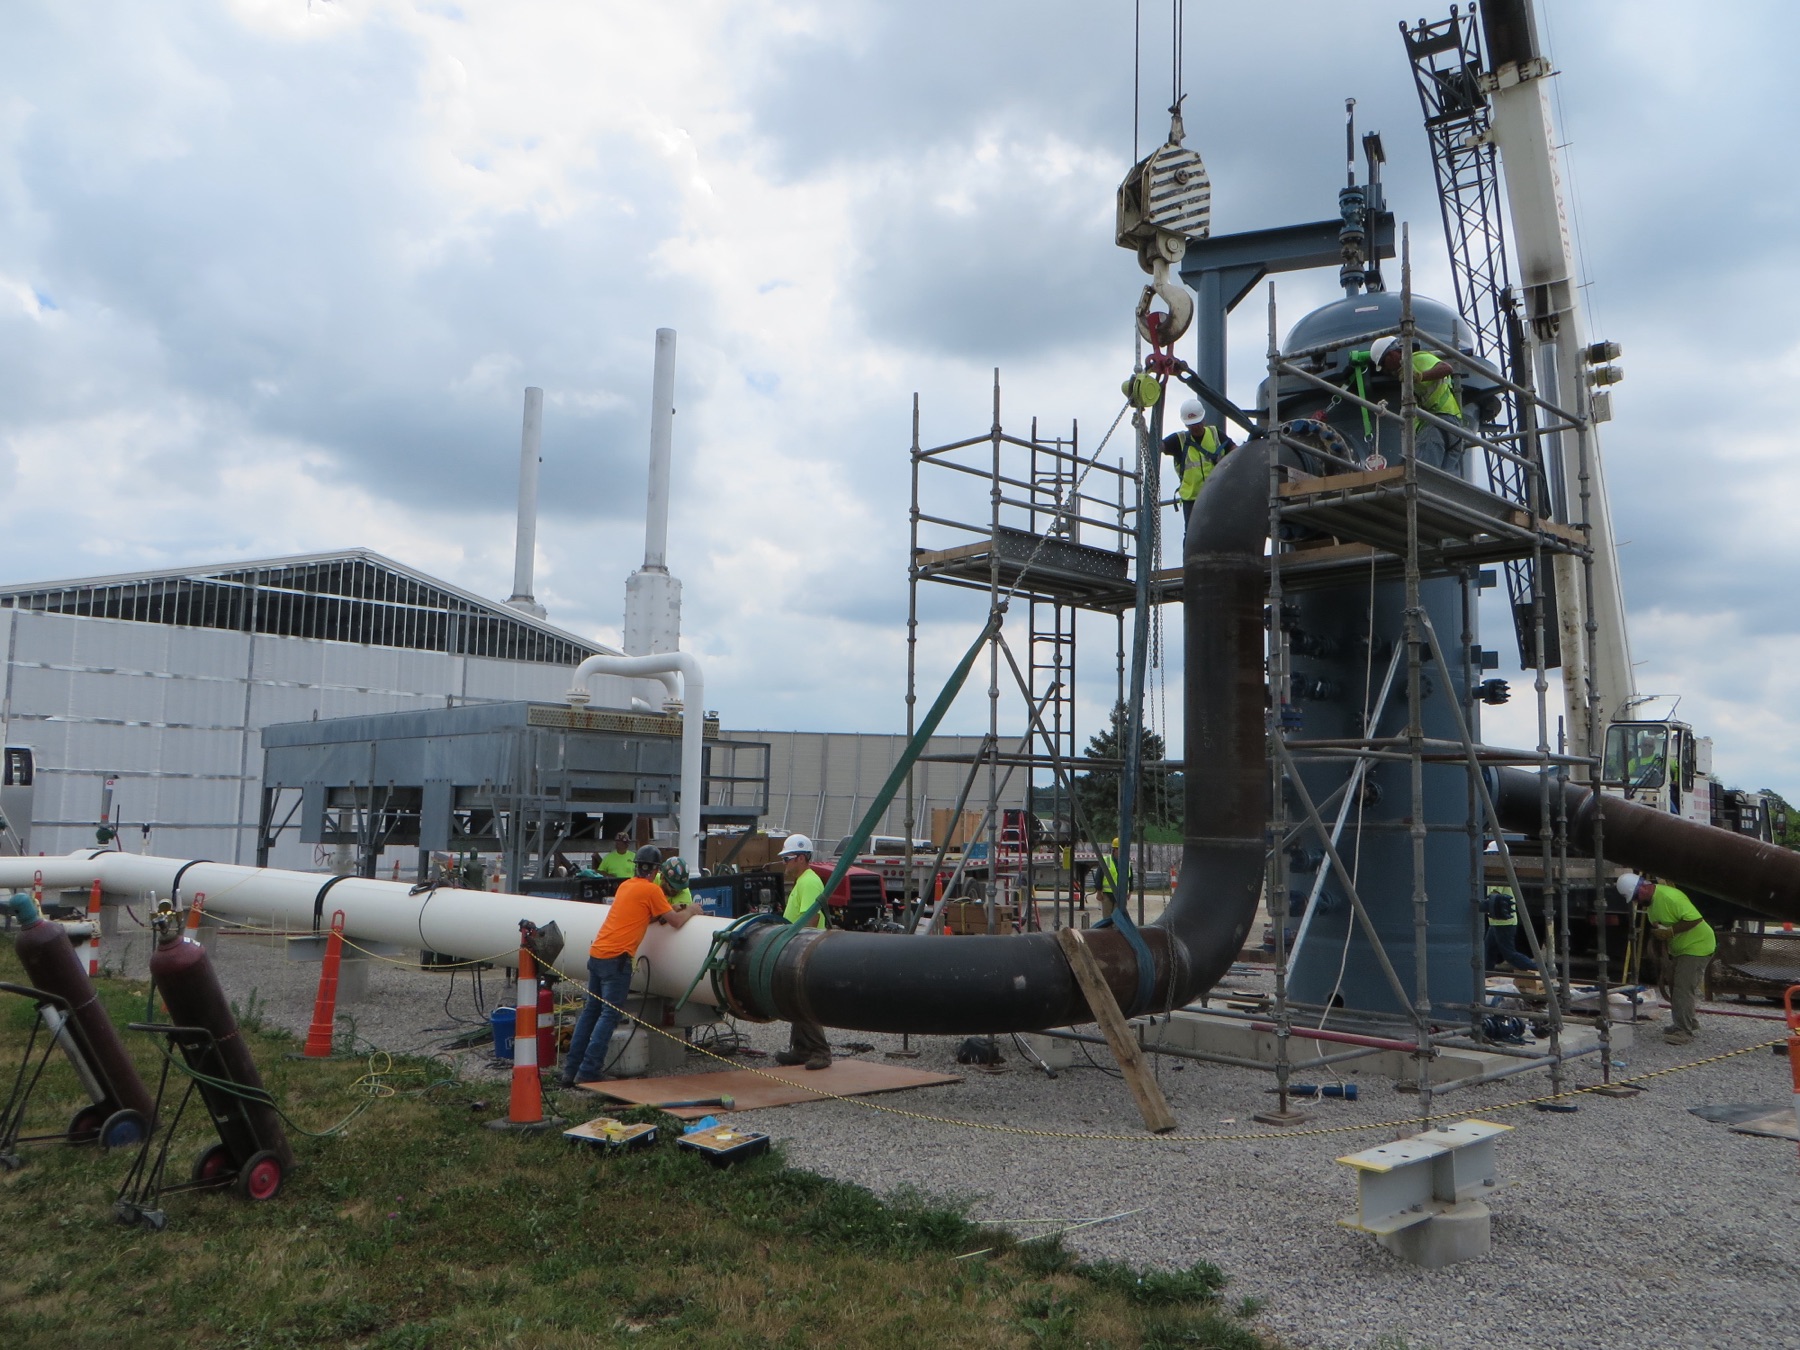
When the spools arrived onsite at the compressor station, they were hoisted into place for install, and required only a single field weld with zero field modifications. The proper tolerance for the joint fit up is 1/16” for a GTAW “TIG” Root. Without this unique combination of Egan’s construction technology and fabrication services, the project foremen estimated that this project would have required multiple weeks to field erect a series of connections. Instead, Egan completed this installation in just three days. In fact, the customer was able to add scope during this planned shutdown without pushing out the project schedule. By keeping onsite hot work to absolute minimum, Egan also created an overall safer environment, minimizing risk on this very unique project.
More in Power.
Let's build it right.
When quality counts, Egan is the industry-leading, single-source mechanical contractor with the experience, technology and capacity for projects with the most rigorous construction standards.
24/7 Emergency Service · 1-800-594-9244